Critical spares in maintenance planning exist for one reason: to make recovery predictable. The scenario that exposes facilities most acutely is not the common fault with a stocked replacement - it is the failed component that is no longer manufactured, no longer supported, and no longer available at any price.
Siemens, Allen-Bradley, and RDM control systems running UK production lines routinely carry components that entered end-of-life status years ago. Many facilities are unaware of this until a failure forces the issue. At that point, the options narrow considerably - and the costs of resolution escalate sharply.
This article sets out how manufacturer lifecycle signals work, what the different status designations mean for your maintenance risk, and how to build a structured response before a failure forces your hand.
How Manufacturers Signal End of Life - and Why Facilities Miss the Warning
Most major PLC and drive manufacturers follow a documented lifecycle process. Siemens publishes formal Product Discontinuation Notices. Rockwell Automation - the manufacturer of Allen-Bradley equipment - operates a defined lifecycle programme with active, mature, and discontinued product phases. RDM issues similar communications to registered users and channel partners.
The problem is not that the signals are hidden. The problem is that they reach procurement departments, distributor mailing lists, and manufacturer portals - not the maintenance teams responsible for the assets in the field. A facility without a formal process for cross-referencing installed assets against manufacturer lifecycle data will miss these notifications consistently.
Single Points of Failure Carry the Highest Obsolescence Risk
Components with no installed redundancy and no available replacement represent the most acute category of obsolescence risk. These should be identified and prioritised in any lifecycle assessment - because when they fail, there is no fallback position.
Last Time Buy windows - the final purchase period before a component stops being manufactured - are typically open for a defined period, often six to eighteen months. Once that window closes, the only supply is the secondary market, which carries its own risks: uncertain provenance, unknown storage conditions, and no manufacturer warranty.
Without a formal monitoring process, facilities routinely miss these windows entirely. By the time a component fails and the team discovers it is discontinued, the Last Time Buy period closed months or years earlier.
Discontinued, Last-Time-Buy, and Unsupported: What Each Status Means for Your Maintenance Risk
These three terms are often used interchangeably, but they describe materially different risk profiles for the maintenance manager.
- Discontinued - the component is no longer manufactured. New units are unavailable through authorised channels. Supply exists only through secondary market sources, surplus dealers, or cannibalisation from decommissioned equipment. Provenance and condition cannot be guaranteed.
- Last-Time-Buy - the manufacturer has issued a final purchase window. New stock can still be ordered through authorised distributors, but the window is time-limited. This is the last low-risk, traceable opportunity to secure replacement stock at a predictable price.
- Unsupported - the manufacturer has ended technical support, firmware updates, and security patches. The component may still be available to purchase, but there is no remediation path if a software fault, firmware incompatibility, or cybersecurity vulnerability is identified. This status is particularly relevant for networked automation systems.
A component can carry more than one of these statuses simultaneously. An Allen-Bradley PLC module that is both discontinued and unsupported presents a fundamentally different risk profile to a Siemens drive that is last-time-buy but still fully supported. Understanding which status applies - and to which specific catalogue reference - is the foundation of any credible obsolescence risk assessment.
Status Determines Your Response Window
Last-Time-Buy status is an action trigger, not just a status label. A facility that identifies a critical control component in this category has a defined window to make a stocking decision at a known cost. Allowing that window to close without a decision is itself a decision - and the costlier one.
Why Pre-Sourced Obsolete Spares Are Usually Cheaper Than Emergency Redesign
The instinctive reluctance to hold aged spares inventory is understandable. It ties up capital in components that may never be needed. That calculation changes materially once a component reaches end-of-life status and no drop-in replacement exists.
Emergency redesign after an unplanned failure on a discontinued platform carries costs that extend well beyond component price. Engineering time to re-architect the control system accumulates quickly. So does the downtime while that work proceeds. Expedited delivery on replacement hardware and operator retraining both add further cost on top.
Illustrative Scenario — RDM Refrigeration Control System I/O Module
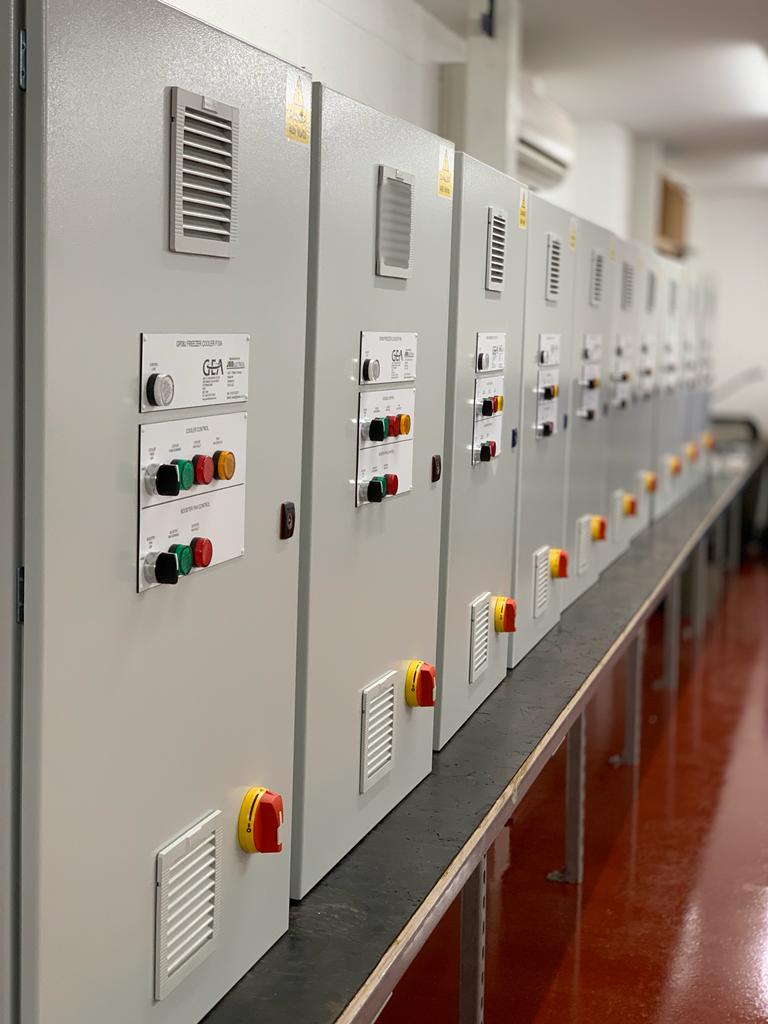
Consider a food manufacturing facility running a legacy RDM refrigeration control system where a critical I/O module enters Last-Time-Buy status. The module controls compressor sequencing across a cold store serving active production. An engineer conducting a lifecycle review would flag this as a single point of failure - no redundancy, no compatible replacement available once the window closes. The engineering response is to procure a defined stock quantity during the Last-Time-Buy window, store with documented installation procedures and configuration backups, and link the holding to the planned maintenance schedule. The consequence avoided is an unplanned compressor trip with no available replacement, and the multi-day production loss while a redesign path is identified and executed.
Illustrative example based on representative JBB project work.
Pre-sourcing within the Last-Time-Buy window delivers a known cost at a predictable price point, with traceable provenance and manufacturer documentation. That is a substantially better position than sourcing from secondary markets under time pressure after a production stoppage.
JBB Electrical's Critical Spares service is structured around this principle - identifying the components where a pre-sourced holding is significantly more cost-effective than the emergency alternatives, and maintaining that inventory with the installation procedures and configuration backups needed for swift restoration.
Building a Component Lifecycle Tracker Linked to Your Maintenance Schedule and Spares Inventory
Most facilities hold an asset register. Fewer maintain a lifecycle tracker that cross-references those assets against manufacturer end-of-life data. The gap between the two is where obsolescence risk accumulates undetected.
A functional component lifecycle tracker requires four linked elements.
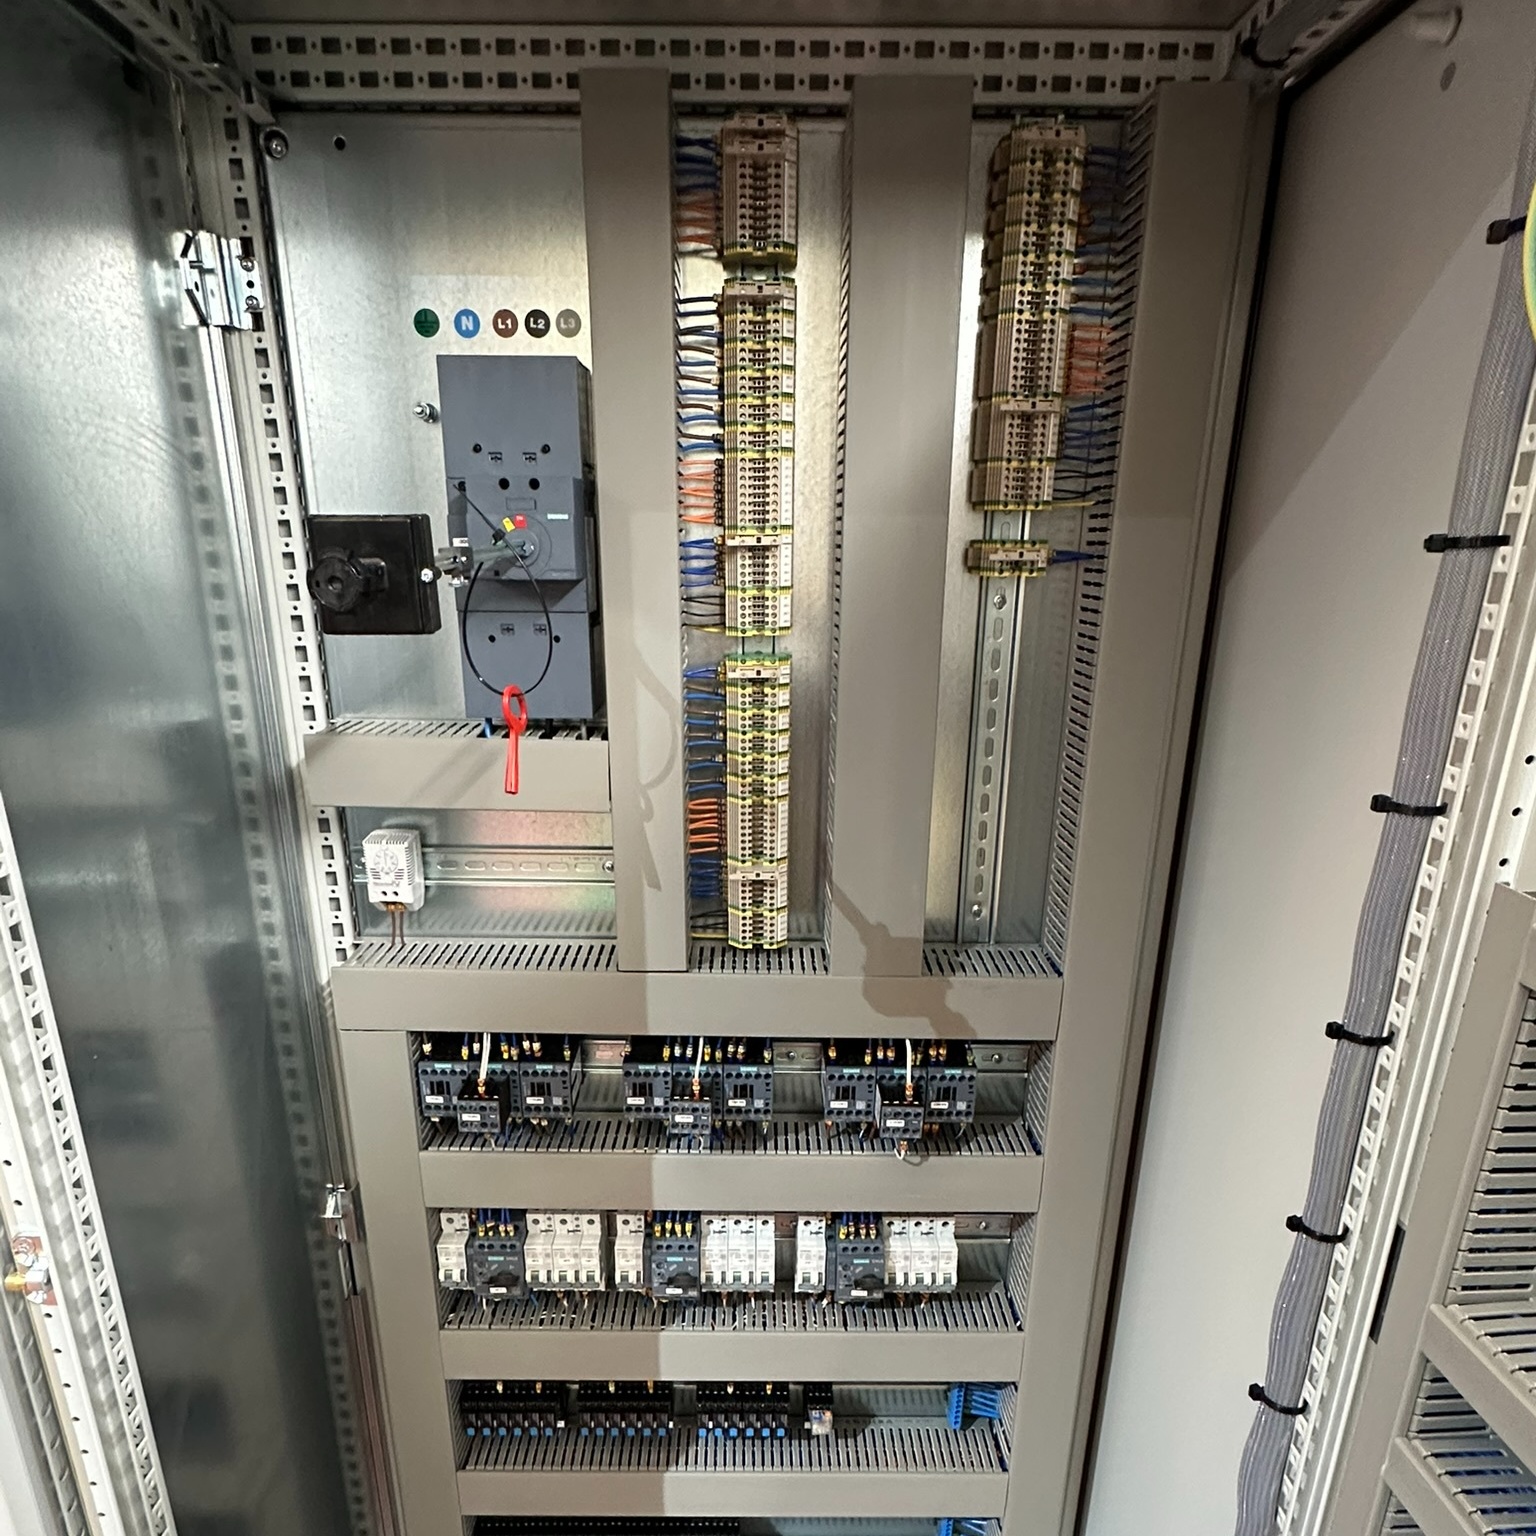
- Installed asset register with catalogue-level detail - not just 'Siemens S7 PLC' but the specific CPU module, I/O cards, power supplies, and firmware version. Lifecycle status varies at catalogue reference level, not product family level.
- Manufacturer lifecycle data mapped to each reference - active, mature, last-time-buy, discontinued, or unsupported. This data is available from manufacturer lifecycle portals and should be reviewed on a defined schedule, not just at point of installation.
- Risk horizon flags - components approaching end-of-life within a defined window (typically 24-36 months) should trigger a formal review: stock decision, redesign assessment, or migration consideration.
- Integration with planned maintenance schedules and spares inventory - lifecycle risk should inform maintenance frequency decisions. A component approaching end-of-life on a system with high failure consequence warrants increased inspection frequency and a confirmed spare holding.
Common Gap: Asset Registers Rarely Capture Catalogue-Level Detail
Most installed asset registers identify equipment at product family level — 'Siemens S7-300 PLC' or 'Allen-Bradley PowerFlex drive' — rather than at the specific catalogue reference. Lifecycle status, however, applies at catalogue reference level. A CPU module and its associated I/O cards within the same product family can carry different lifecycle statuses. Without catalogue-level detail in the asset register, it is not possible to cross-reference against manufacturer lifecycle data accurately, and components already in Last-Time-Buy status will be missed.
This tracker does not need to be a sophisticated software system. A structured register maintained alongside your Preventive Electrical Maintenance programme is sufficient, provided it is reviewed on a scheduled basis and linked to procurement decisions when flags are raised.
Start With Single Points of Failure
If building a lifecycle tracker from scratch, begin with the components that have no redundancy and no straightforward replacement. Map their lifecycle status first. These represent your highest-consequence exposure and will justify the tracking investment most immediately.
The JBB Component Obsolescence Methodology
The JBB Component Obsolescence Methodology
Assess
JBB engineers conduct a catalogue-level audit of installed PLC modules, drives, HMI screens, and control components across Siemens, Allen-Bradley, and RDM platforms, cross-referencing each reference against current manufacturer lifecycle status to identify discontinued, last-time-buy, and unsupported items. As an NICEIC-approved contractor, this assessment is carried out to a documented standard with a structured output - not a verbal walk-around.
Modernise
Where lifecycle assessment identifies components where continued obsolescence management is no longer viable - typically due to unavailability of spares, escalating failure frequency, or loss of manufacturer firmware support - JBB engineers scope migration options using EPLAN Electric P8 for control architecture redesign, covering Siemens, Allen-Bradley, and RDM replacement pathways.
Protect
For components still within a viable stocking window, JBB's intelligent engineering approach identifies the minimum strategic holding required to protect against unplanned downtime, procures within the Last-Time-Buy window where applicable, and stores with full installation procedures, commissioning checklists, and configuration backups specific to each asset.
Prevent
Component lifecycle data is integrated into planned maintenance schedules through JBB's Critical Spares Strategy programme - linking risk horizon flags to inspection frequency decisions, so deteriorating components on end-of-life platforms are identified before they fail rather than after. Founded 1966, JBB brings decades of platform-specific experience to this predictive layer.
Support
JBB provides ongoing lifecycle monitoring as part of the same team that designed, built, and documented the spares strategy - eliminating the accountability gaps that arise when design, manufacture, and installation are divided between different contractors. Inventory is reviewed on a scheduled basis with proactive replacement scheduling as components approach end of serviceable life.
When Obsolescence Risk Becomes the Trigger to Migrate Rather Than Stock
Stocking aged spares is a viable strategy - until it is not. The decision to migrate a legacy PLC system rather than continue managing obsolescence risk through inventory should be driven by specific, identifiable criteria, not a general preference for newer technology.
Engineering Necessity, Not Technology Preference
The decision to migrate should never be driven by a general preference for newer hardware or a manufacturer's product roadmap. It is an engineering decision, triggered by specific and measurable conditions in your facility. When those conditions are not met, continued obsolescence management through structured inventory and lifecycle monitoring is the correct response. When they are met, migration becomes the lower-risk and frequently lower-cost path — but only when planned, not when forced by an unplanned failure.
Migration becomes the considered response when the cost and risk of continued stocking exceeds the cost of planned transition. That threshold is reached when one or more of the following conditions apply.
Modelling the Three-to-Five Year Horizon
The comparison between continued stocking and planned migration is most reliably made over a three to five year horizon. Cumulative obsolescence management costs — inventory holding, secondary market sourcing at premium prices, third-party repair, and the probability-weighted cost of extended downtime — are totalled and set against the cost of a planned migration executed during a scheduled shutdown. Over that horizon, migration frequently becomes the lower-cost option. Without this modelling, the decision defaults to inertia, and the facility reaches the forced-migration endpoint under significantly worse conditions.
- Spares are no longer available at any price - the Last-Time-Buy window has closed. Secondary market supply is exhausted or unreliable. No compatible replacement exists. A single failure becomes a forced migration under the worst possible conditions.
- Failure frequency is escalating - multiple failures in a short period on the same platform indicate systemic deterioration. Managing each failure individually may cost more than a planned migration over a defined horizon.
- Manufacturer support has ended entirely - an unsupported platform with no firmware path carries escalating risk as connected systems are updated around it. There is no remediation route if a software fault or vulnerability is identified.
- Total obsolescence management cost exceeds migration cost - when inventory holding, secondary market sourcing, third-party repair, and extended downtime risk are modelled together, planned migration frequently becomes the lower-cost option over a three to five year horizon.
Migration in this context is not a technology preference - it is the rational response to a specific set of conditions. JBB's PLC & Software Development service supports this transition when it becomes the right decision, covering redesign, reprogramming, and integration across the same Siemens, Allen-Bradley, and RDM platforms where lifecycle risk is most commonly concentrated in UK industrial facilities.
Planned Migration Is Categorically Different From Forced Migration
A facility that identifies migration criteria being met and plans the transition during a scheduled shutdown retains control of scope, cost, and timeline. A facility that reaches the same endpoint via an unplanned failure - with no available spare and no migration plan prepared - faces the same engineering work under substantially worse conditions, typically including extended production loss.
Next Step: Request a Compliance & Breakdown Prevention Assessment
Next Step: Request a Compliance & Breakdown Prevention Assessment
A Compliance & Breakdown Prevention Assessment identifies the electrical, compliance, and breakdown risks affecting your operation, and sets out the engineering actions needed to reduce downtime, protect reliability, and keep your infrastructure defensibly compliant. Request a Compliance & Breakdown Prevention Assessment today to establish which components in your Siemens, Allen-Bradley, or RDM control systems are approaching end-of-life - and to put a structured spares and migration strategy in place before a failure forces the decision.
Compliance & Breakdown Prevention Assessment